Sourcing & Supply
Supplier Capacity Assessment: Verify Production Slots Before Placing an Import Order
20 Oct 2026 · 18:03 CET
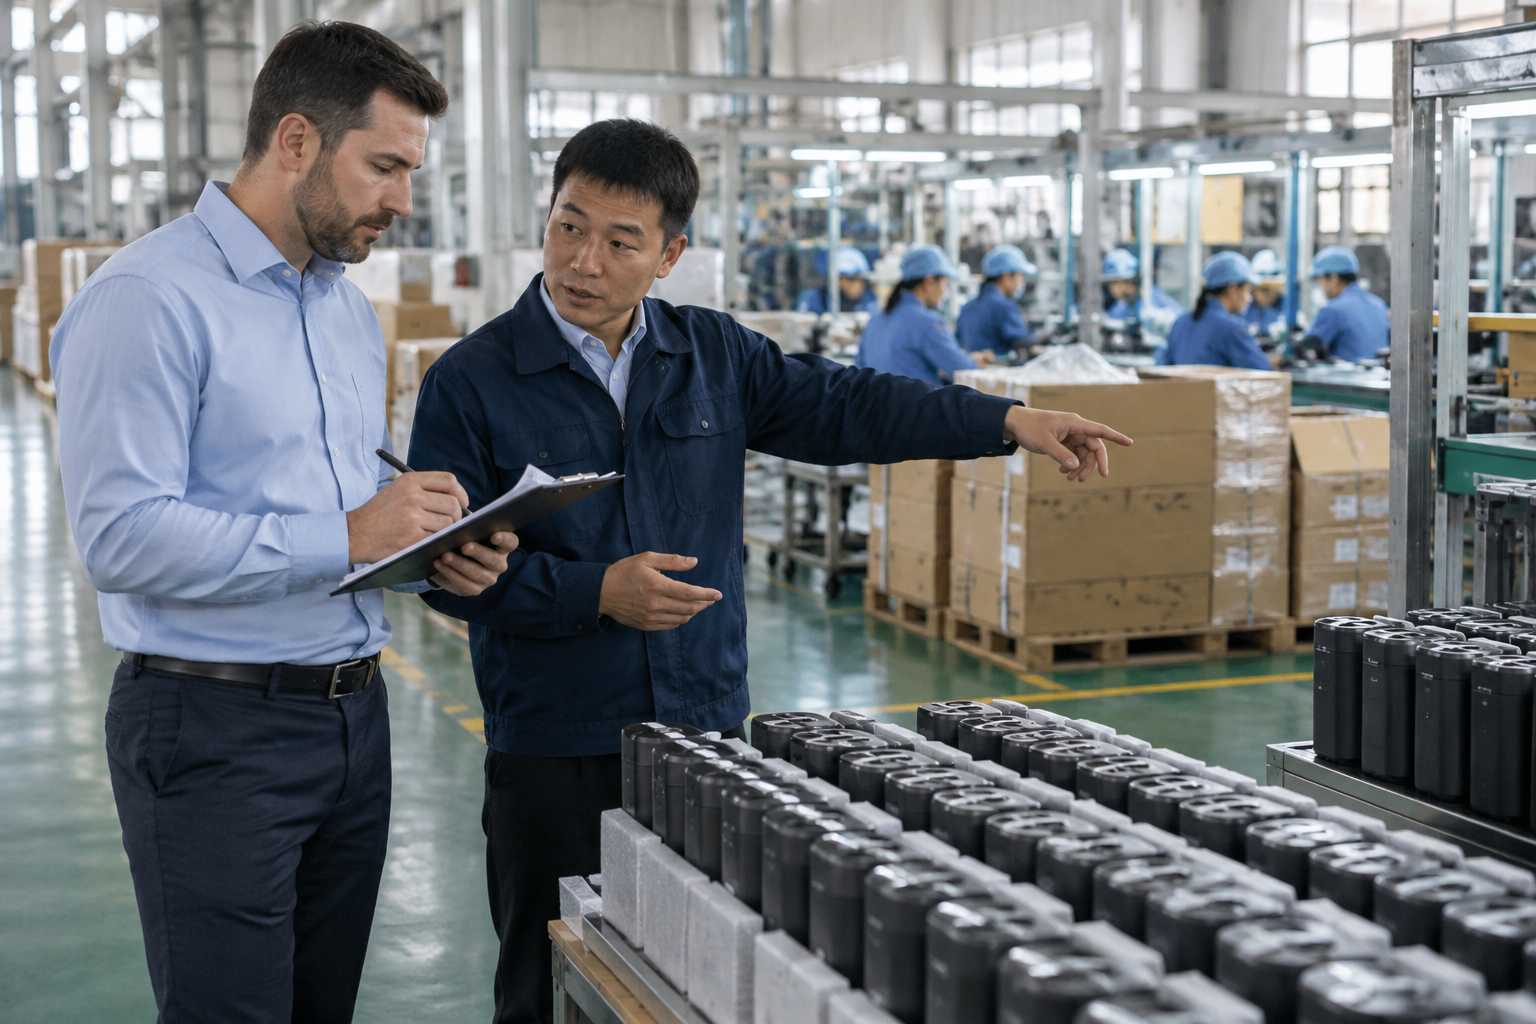
A supplier capacity assessment answers a question that company registration documents and product catalogues cannot: can this supplier manufacture your specified quantity within the production window your import order requires? A legitimate factory may still lack available machine time, trained workers, materials or approved subcontractors when you need them.
For importers, the objective is not to confirm theoretical monthly output. It is to establish whether a realistic, order-specific production slot exists—and turn that finding into documented commitments before paying a deposit.
Why advertised output is not available capacity
A supplier’s headline output may describe ideal conditions: uninterrupted operation, a familiar product, full staffing and no material shortages. Your order may require slower processing, additional changeovers or more demanding inspection.
Existing orders can consume the same resources your goods need. Maintenance, tooling changes, holidays and rework can further reduce usable time. A factory with spare assembly capacity may still have no available coating, testing or packaging capacity.
Separate three concepts:
- Theoretical capacity: maximum output under stated assumptions.
- Demonstrated capacity: output achieved for comparable products under normal operating conditions.
- Available capacity: capacity remaining for your order after existing commitments and operating constraints.
Ask which figure the supplier is quoting. A factory-wide monthly number is not evidence that a specific line, process or production team is reserved for you.
Define the delivery requirement before requesting offers
Capacity cannot be assessed against an incomplete brief. Before approaching suppliers, the buyer’s sourcing lead should align specifications and timing with quality, logistics and commercial teams.
Include these requirements in the request for quotation:
- Order quantity by product, variant and batch.
- Production-ready drawings, materials, tolerances and packaging requirements.
- Required samples, approvals, testing and inspection stages.
- Required goods-ready date and shipment or arrival deadline, clearly distinguished.
- Delivery term and named place, where applicable.
- Whether split deliveries are acceptable, including minimum useful quantities.
- The deadline for resolving technical questions and approving samples.
If specifications remain open, ask for a conditional schedule that identifies every assumption. Do not treat that schedule as a confirmed production commitment.
Work backwards from the required delivery event. Allow time for inspection, corrective work, packing, booking, transport and any applicable customs clearance—not only manufacturing. The buyer’s logistics owner should validate these allowances before the sourcing team accepts the supplier’s proposed goods-ready date.
Supplier capacity assessment checklist: evidence before deposit
Request a concise, order-specific evidence pack. Suppliers can redact customer names, pricing and other confidential details while retaining enough scheduling information to support a meaningful review.
Production allocation and existing workload
Ask for a proposed production window showing the relevant line or work centre, planned start and finish, and quantity allocated to each batch. Request a redacted load plan covering that window.
The plan should distinguish confirmed orders from tentative reservations. Ask what event secures your allocation, how long the offer remains valid and whether another order could displace it before acceptance. If the seller is a trading company, identify the actual manufacturing site and obtain evidence supporting its allocation there.
Bottleneck capacity and realistic output
Identify the operation that limits throughput: machining, moulding, finishing, assembly, testing or another process. Request its planned operating hours, output rate for comparable products, changeover requirements and expected quality losses.
Recent production records can help substantiate these assumptions. Check whether reported output means units started, units completed or accepted units ready for shipment.
Material and tooling readiness
Request a material readiness list showing critical components, stock available for allocation, outstanding purchases, expected receipt dates and incoming inspection requirements.
“Materials available” is insufficient if the stock is already committed elsewhere. Confirm whether tooling exists, whether it needs modification and who must approve it before production can begin.
Planned subcontracting
Ask which operations, if any, will be outsourced. Identify the proposed subcontractor, location, capacity evidence, quality controls and transfer time.
Subcontracting is not automatically a problem. Undisclosed subcontracting creates uncertainty about schedule control, traceability and accountability. Require advance disclosure and an agreed approval process for changes.
How to verify supplier production capacity against the schedule
A credible schedule connects quantities, resources and dependencies. It should explain how the supplier moves from material receipt to accepted, packed goods—not merely show a start date and a shipment promise.
Check the limiting operation
Start with the bottleneck rather than the fastest machine. A useful screening calculation is:
Estimated available accepted output = uncommitted operating hours × demonstrated units per hour × expected acceptance yield.
Use realistic hours remaining after booked work, maintenance and changeovers. Express yield as a proportion. Apply a yield adjustment only if the production rate does not already represent accepted output; otherwise, losses would be counted twice. Keep the time and rate assumptions consistent so downtime is neither overlooked nor deducted twice.
Compare the result with your required quantity in the relevant window. Then check whether upstream and downstream operations can support that flow. Shared tooling, specialist operators or inspection equipment may create constraints that a machine-only calculation misses. This calculation screens feasibility; it does not prove that capacity has been reserved.
Separate production time from total lead time
Supplier lead time verification should cover the full sequence:
- Specification and sample approval.
- Material purchasing, receipt and acceptance.
- Tool preparation and line setup.
- Manufacturing and any subcontracted operations.
- Inspection, rework, packing and release.
- Handover for the agreed shipment arrangement.
Ask when each clock starts. A quoted lead time measured from deposit receipt is different from one measured from the availability of all materials and approvals. Identify which activities can overlap and which must finish before the next begins.
Test disruption scenarios
Ask what happens if a critical material is late, a machine stops or first-pass quality falls below the plan. Identify the recovery option, its owner and the time required to activate it.
A schedule dependent on continuous overtime, unapproved outsourcing or perfect yields needs further evidence. Resolve the gap through an earlier material release, smaller first shipment, revised deadline or alternative supplier—not an unsupported promise to work faster. Any overtime plan should comply with applicable working-time and safety requirements.
When an independent manufacturing capacity audit is warranted
Consider an independent manufacturing capacity audit when the order is commercially critical, the process is unfamiliar, evidence is inconsistent or the supplier cannot explain its scheduling assumptions.
Give the assessor an order-specific scope: inspect relevant equipment, review redacted load records, examine bottleneck performance, check material status and evaluate proposed subcontracting. Request findings tied to your quantity and production window, with limitations clearly stated.
A site visit cannot guarantee future delivery or reveal every competing commitment. Its value lies in testing whether the proposed plan is supported by observable resources and credible records. The buyer’s sourcing lead should close significant capacity findings before authorising the deposit.
Compare candidates through IMEX Center
When evaluating suppliers found through IMEX Center, treat company information as a starting point for discovery, not proof of available capacity, product conformity or future delivery. Check what any verification label actually covers rather than assuming it includes factory operations.
Prepare a sourcing brief with your quantity, specification status, required goods-ready date and acceptable split-delivery conditions. Share the same requirements with each candidate so their responses are easier to compare.
Use written communications to clarify capacity assumptions, request supporting evidence and resolve ambiguous dates. Where communications involve translation, have critical technical terms checked by a competent reviewer. Restate agreed dates explicitly, then capture them in the commercial documentation.
Compare candidates on more than price:
- Evidence supporting the proposed production slot.
- Credibility of bottleneck and material assumptions.
- Transparency about existing workload and subcontracting.
- Quality of the recovery plan.
- Willingness to document responsibilities and milestones.
The buyer remains responsible for due diligence and the purchasing decision. Platform discovery and communication do not replace order-specific verification.
Turn capacity discussions into specific commitments
Summarise the proposed arrangement in a written term sheet or draft agreement for incorporation into the final contract. Do not assume preliminary notes alone provide sufficient contractual protection; obtain appropriate review of the final terms before signing or paying a deposit.
Document:
- Production allocation: product, quantity, site, relevant line and agreed production window.
- Dependencies: buyer approvals, material availability and the conditions that start lead time.
- Milestones: material readiness, production start, batch completion, inspection and goods-ready dates.
- Subcontracting controls: disclosed operations and approval requirements for changes.
- Reporting duties: named contacts, evidence required and reporting frequency.
- Delay notification: the notification deadline after a risk is identified and the required recovery proposal.
- Remedies: agreed treatment of partial shipments, expediting costs, cancellation or refunds, subject to final contractual terms and applicable law.
Delivery commitments should identify measurable events. Replace “delivery as soon as possible” with defined dates, responsibilities and escalation steps. Distinguish goods-ready, carrier handover and destination arrival, and identify who controls each event.
Assign follow-through before signing
The sourcing lead owns capacity-gap resolution before deposit approval. The supplier’s production contact confirms material readiness before production starts and reports against agreed milestones.
The buyer’s quality owner confirms inspection criteria before production release. The logistics owner checks booking requirements before accepting the goods-ready plan.
At each milestone, request evidence proportionate to risk: material receipt records, batch output reports, inspection results or an independent check. If progress slips, require a revised schedule showing the remaining bottleneck workload, recovery actions, deadlines and accountable owners before approving further payment where the agreement permits.
FAQ
What is the difference between a supplier audit and a capacity assessment?
A supplier audit may examine broader business, quality or operational controls. A capacity assessment focuses on whether resources and available production time can support your specific quantity and schedule. An audit supports that decision only if its scope addresses those questions.
How can a supplier protect confidential customer information?
The supplier can redact customer identities and commercial terms while showing booked hours, process loads and available slots. An independent assessor can review sensitive records and report findings subject to agreed confidentiality arrangements.
Does a verified company profile guarantee production capacity?
No. Company verification does not by itself establish that a production slot, materials or subcontractor capacity are available for your order. Check the scope of verification and obtain separate, current capacity evidence and documented commitments.
Should an importer pay a deposit before capacity is confirmed?
Avoid paying against an unexplained capacity promise. If a deposit is needed to reserve materials or a slot, first document the allocation mechanism, reservation conditions, confirmation deadline, milestones and agreed treatment of a failure to secure them. Assess the remaining payment risk before proceeding.
Source with clearer production commitments
Ready to compare suppliers? Explore IMEX Center and prepare a sourcing brief that specifies quantity, production requirements and delivery milestones. Buyers should request order-specific capacity evidence; suppliers should provide it alongside company and product information. Make the documented production slot—not advertised output—the basis of the agreement.
Source or sell globally with IMEX Center
Browse verified suppliers →