Sourcing & Supply
Supplier Factory Audit: Who Will Actually Make Your Order?
02 Oct 2026 · 14:02 CET
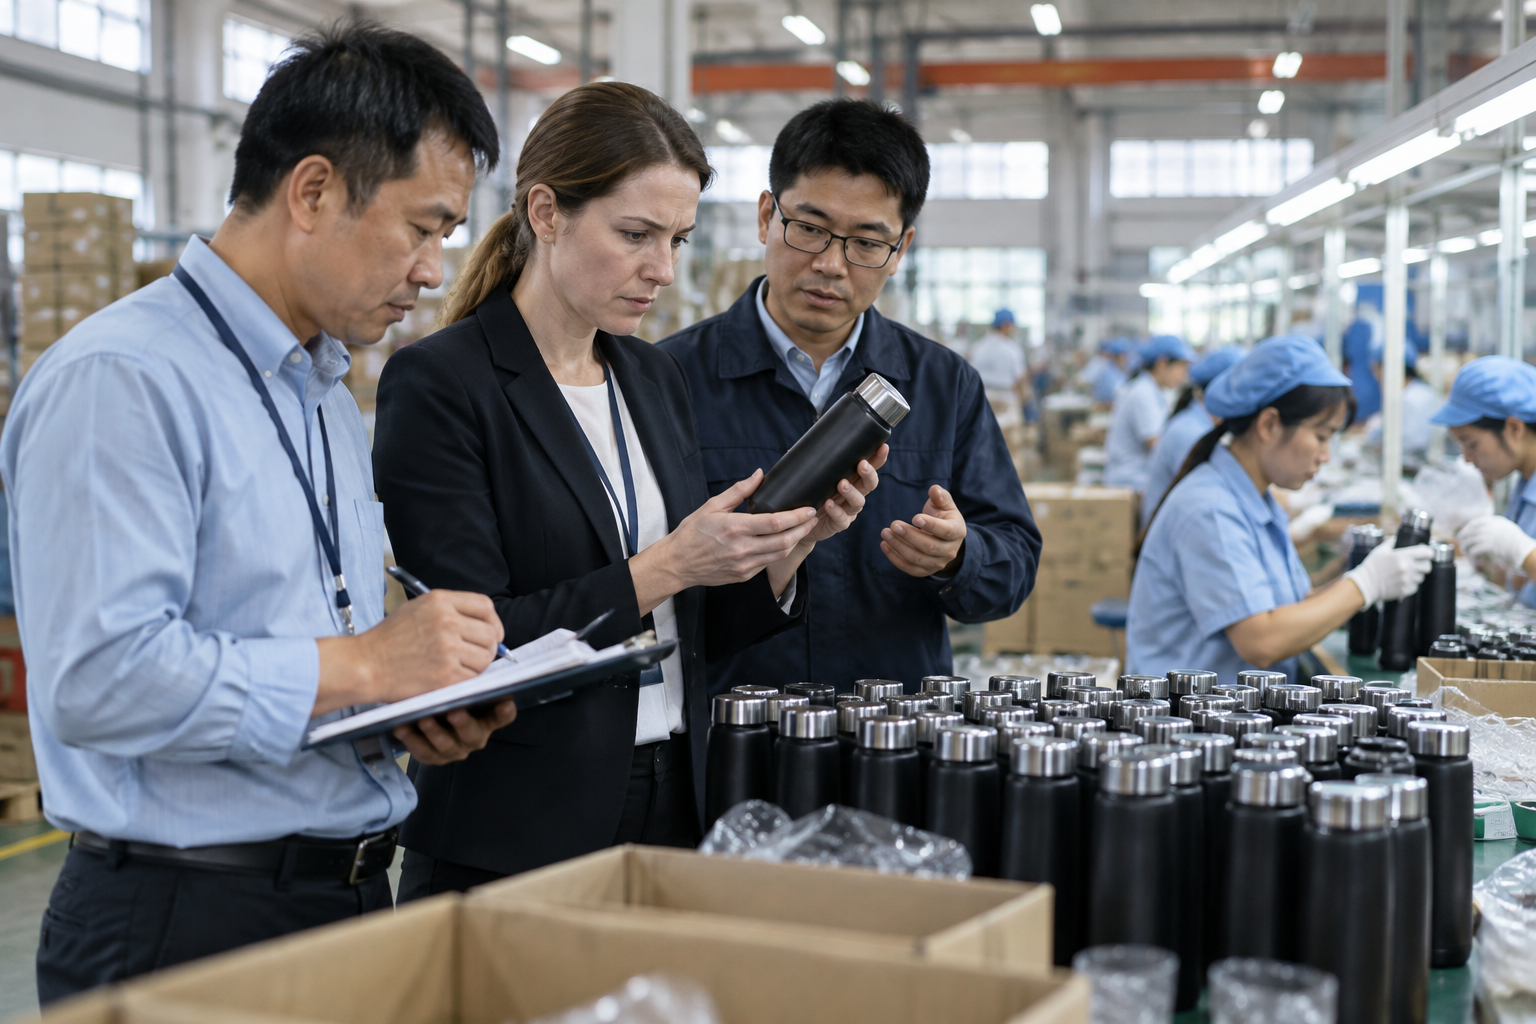
A supplier factory audit should answer a question that a business registration check cannot: who will actually manufacture your order? For importers evaluating an overseas supplier, confirming that a company exists is only the beginning. The purchasing decision depends on whether the proposed production network can meet your specifications, quality requirements, and agreed schedule.
An approved sample may come from a development workshop, a specialist subcontractor, or a different factory from the one handling bulk production. Without visibility into that handoff, buyers can approve one manufacturing arrangement and unknowingly receive goods from another.
The goal is not to eliminate outsourcing. It is to make production responsibilities visible, test the evidence, and establish approval conditions before committing to an order.
What a Supplier Factory Audit Must Establish
Start by separating three roles that may belong to different businesses:
- Contracting entity: the company signing the purchase agreement and accepting the obligations set out in it.
- Factory operator: the business running the site where manufacturing will occur.
- Subcontractor: any outside business performing production, processing, assembly, or other relevant work.
A trading company can be a capable supplier without owning a factory. Conversely, factory ownership does not demonstrate that a particular order will be produced there or that the site has suitable capacity.
Build an entity-to-site record
Request the legal names, physical addresses, and roles of the seller, proposed factory operators, and critical subcontractors. Record which entity controls equipment, employs production staff, and maintains quality records.
Compare these details across quotations, contracts, available registration documents, audit reports, and production records. Ask the supplier to explain discrepancies rather than assuming that a shared brand name means shared ownership.
Your output should be a clear chain from the company accepting the order to the sites performing the work.
Start With IMEX Center Profiles, Then Verify Production Claims
Use supplier profiles on IMEX Center as a starting point for discovery and preliminary research. Review the available information. If a profile displays a verification label, read the stated scope before deciding what that label establishes.
A verification label alone is not proof of factory ownership, production capacity, or subcontractor oversight. Do not extend a verification claim beyond the checks explicitly described. If the scope is unclear, seek clarification and treat production claims as unconfirmed.
For each shortlisted supplier, create an evidence log:
- What does the supplier claim about its manufacturing role?
- Which entity and address does the available information identify?
- Is a verification scope stated, and what does it cover?
- Which claims require independent documentation or site-level checks?
- What remains unresolved before approval?
Overseas factory verification should connect identity evidence with operational evidence. A registered address may be an office rather than a production facility. Product photographs and machinery lists are useful discussion prompts, but they do not establish who controls the equipment or where your order will run.
Request a Production Map Before Booking the Audit
Ask the supplier to map your product from incoming materials to finished-goods dispatch. A production map should identify each major process, its location, its operator, and the associated quality checks.
Include outsourced steps that are easy to overlook, such as coating, heat treatment, printing, testing, or final packing. Identify critical component sources where substitution could affect fit, performance, safety, or delivery.
Production-map checklist
For each important step, record:
- The process and its significance to product conformity.
- The site name, address, and operating entity.
- Whether the process is in-house or outsourced.
- The required equipment, tooling, and workforce skills.
- The inspection point and person responsible for acceptance.
- The records linking inputs, batches, and finished goods.
- Any proposed alternative site or component source.
Use this map to determine audit coverage. Visiting an assembly site alone may leave the highest-risk process unexamined if a separate facility performs it.
A supplier that cannot explain where critical work occurs is not ready for unconditional production approval.
Audit Capability Against Your Specific Order
To assess manufacturing capability, focus on the proposed product and process—not the factory's appearance or its broad category experience. A site may make similar goods while lacking the tolerances, material controls, or testing capability your order requires.
Provide the auditor with your specifications, proposed quantity, delivery requirements, production map, and known concerns. Confirm access to the actual manufacturing areas and relevant records, subject to reasonable confidentiality protections. A capability audit does not replace any required product testing, certification, or regulatory compliance assessment.
Factory audit checklist
Check for evidence in these areas:
- Equipment: suitability for required processes, operating condition, maintenance records, and available tooling.
- People: trained operators, process supervision, and quality staff with clear responsibilities.
- Production history: relevant work orders, batch records, and inspection results tied to the audited site.
- Material controls: receiving checks, storage conditions, identification, and prevention of unauthorized substitution.
- Quality controls: defined acceptance criteria, appropriate measuring equipment, calibration records where applicable, and treatment of nonconforming goods.
- Traceability: links between incoming materials, work in progress, inspection results, and finished batches.
Test capacity at the bottleneck
The capacity assessment should examine the slowest critical process, not simply count machines. Request evidence for cycle times, staffing, shifts, changeovers, maintenance downtime, yield, and existing commitments.
Distinguish theoretical output from demonstrated usable capacity. Ask how your order fits into the current schedule and whether the delivery promise depends on overtime, additional equipment, or outsourced overflow.
A factory visit is a snapshot, not a delivery guarantee. Where scheduling remains uncertain, require an evidence-backed production plan and, where appropriate, a trial run before increasing your commitment.
Trace the Approved Sample to Bulk Production
Sample approval supports a production decision only to the extent that you understand how the sample was made and what will change during bulk manufacturing.
Ask whether the approved sample used the intended production site, materials, tooling, process settings, and inspection methods. A hand-finished development sample may demonstrate design potential without proving repeatable production.
Document the sample's origin and retain an identifiable approved reference together with the specification and acceptance criteria. Record any differences between the sample process and the proposed bulk process.
Before authorizing bulk production, confirm:
- The bulk-production site matches the approved arrangement.
- Material grades and critical component sources are agreed.
- Tooling and process changes have been reviewed.
- Work instructions reflect the approved specification.
- A production-intent first article or pilot batch has been assessed where appropriate.
Undisclosed subcontracting can break this chain. If a different factory receives only a photograph or an incomplete specification, your sample approval may never translate into effective production instructions.
Define which changes require review rather than relying on the supplier's assurance that the finished product will look the same.
Distinguish Legitimate Outsourcing From Hidden Risk
Outsourcing can provide specialist capability that the main factory does not need to maintain internally. The concern is whether the arrangement is disclosed, controlled, and accessible for verification.
Supplier subcontracting risks increase when the seller cannot identify the outside processor, explain its quality controls, or provide evidence of acceptance checks. Refusal of reasonable inspection access should be treated as an unresolved approval issue, not automatically as proof of wrongdoing.
Assess control and shared dependencies
For critical subcontractors, establish:
- Who approves their processes and monitors performance.
- What specifications and acceptance criteria they receive.
- How incoming and returned batches are identified.
- Whether inspection and record-review access can be arranged.
- How defects, delays, and corrective actions are communicated.
- Whether further subcontracting is permitted and controlled.
Also investigate shared dependencies. Two shortlisted suppliers may use the same critical processor or component source. They may therefore provide less operational diversification than their separate company names suggest.
Ask about contingency arrangements, but verify proposed alternatives before treating them as approved backup capacity.
Turn Findings Into Supplier Approval Conditions
An audit report should support a purchasing decision, not merely document a visit. Separate verified facts, supplier statements, evidence gaps, and corrective actions. Note the audit's scope, limitations, and any areas that could not be assessed.
Use outcomes such as approved, conditionally approved, or not approved, with reasons tied to your product and order. Assign every required action an owner, required supporting evidence, and a deadline before the relevant production activity.
Document the operating boundaries
In the purchase agreement or associated quality agreement, address:
- Authorized production sites and permitted process allocations.
- Approval requirements for manufacturing subcontractors.
- Prior notification and approval of specified site, process, material, or source changes.
- Agreed inspection access and record availability, including how access to relevant subcontractors will be secured.
- Traceability and record-retention expectations.
- Corrective-action requirements and evidence for closing findings.
- Responsibilities for nonconforming goods and unauthorized production changes.
Have appropriate legal advisers review contractual terms for the transaction. The commercial objective is straightforward: the manufacturing arrangement you assessed should be the arrangement used for your order.
If critical evidence remains unavailable, delay approval until it is resolved. For lower-risk uncertainties, consider a limited initial commitment with defined controls. Do not allow an attractive quotation to substitute for production visibility.
Frequently Asked Questions
Does a verified supplier profile prove factory ownership?
Not by itself. Read the stated verification scope and supporting evidence. Use supplier profiles on IMEX Center for initial discovery, then independently establish factory ownership or operating relationships, production capability, and subcontractor controls where relevant.
Can a trading company pass a supplier factory audit?
Yes, if the assessment covers its actual manufacturing partners and control arrangements and they meet the buyer's defined criteria. A trading company need not own the factory, but it should disclose production sites, demonstrate effective oversight, and facilitate agreed verification access.
Is a remote audit enough before placing an order?
That depends on product risk and evidence quality. Remote document reviews and live walkthroughs can support screening, but they may leave gaps in site access, process observation, and record verification. Use on-site assessment when unresolved risks warrant it.
Should every subcontractor receive a separate audit?
Not necessarily. Prioritize processes that strongly affect conformity, traceability, or continuity. Assess lower-risk activities through proportionate evidence, while requiring deeper checks where failures would be difficult to detect or costly to correct. Follow any applicable regulatory or customer-specific audit requirements.
Source With Better Production Visibility
A sound sourcing decision connects supplier identity, actual manufacturing locations, demonstrated capability, and documented production controls.
Explore suppliers on IMEX Center to begin your shortlist, then validate the manufacturing claims that matter to your order. If you supply B2B buyers, prepare clear evidence of your production role, capabilities, and subcontracting arrangements for your business profile and buyer reviews.
Source or sell globally with IMEX Center
Browse verified suppliers →